
ALL FROM ONE SOURCE.
ALL FROM ONE SOURCE.


Cameras for Inspection
CMOS Camera Models for Inspection for capturing near-infrared (NIR) images with high frame rates and an additional super high dynamic range mode (HDR) of up to 140dB being mapped to true 16bit output. An additional shutter time stamping delivers microsecond precision and a shutter synchronised ADC channel with 16bit resolution is also available.
ReconFlexTM 1920NA
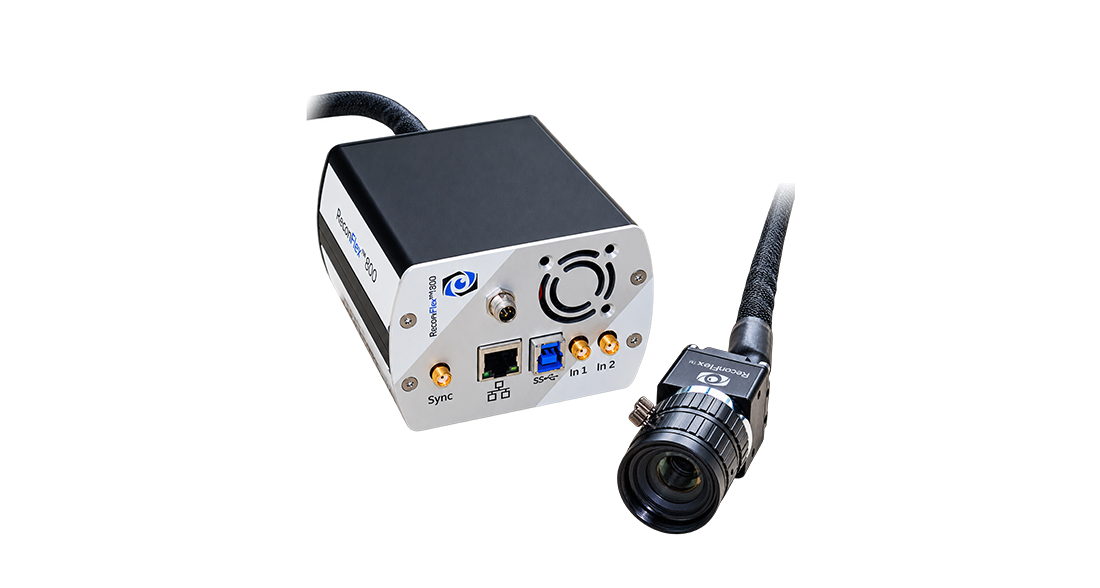
A 2.8-megapixel global-shutter camera that captures NIR images with high frame rates of up to 400fps in full frame mode and more than 2500fps at reduced line number operations.
- Small sensor head (30 x 30 x 30 mm³)
- C-Mount or CS-Mount compatible
- NIR 700nm – 1250nm
- Up to 400fps full frame
- HDR 140dB to true 16bit output
- Exchangeable wavelength filters
- Gbit LAN and USB 3
ReconFlexTM 800NA
A 0.5-megapixel global-shutter camera that captures NIR images with high frame rates of up to 1500fps in full frame mode. In HDR range it reaches up to 140dB, being mapped to true 16bit output with an unmatched 100fps in full frame mode.
- Small sensor head (30 x 30 x 30 mm³)
- C-Mount or CS-Mount compatible
- NIR 700nm – 1250nm
- Up to 1500fps full frame
- HDR 140dB to true 16bit output
- Exchangeable wavelength filters
- Gbit LAN and USB 3
MORE INFORMATION
Welding Process from Camera Side
No contrast stretching or retouching applied.
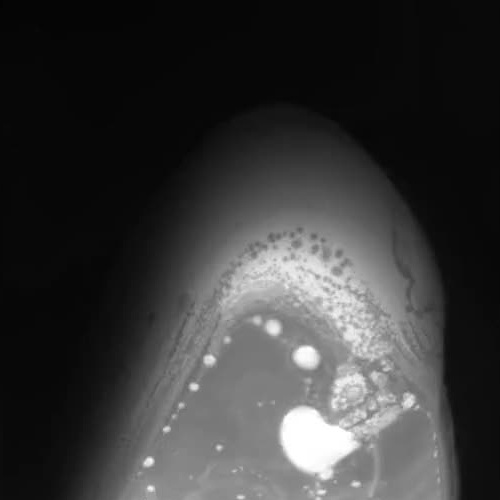
Pool Solidification
At the trailing end of the pool the solidification front travels along with the torch. The boundary between the liquid and the solidified metal stays sharp for the whole recording, and bright particles drifting on the pool surface can be followed until they are captured by the advancing front.
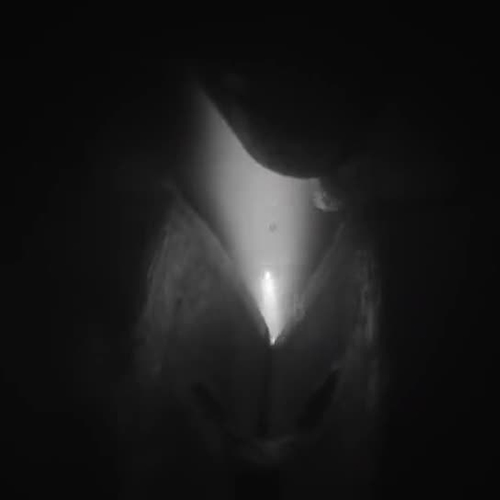
Narrow-Gap Welding
Deep in a narrow gap there is very little light beside the arc itself. The flanks still stay readable, and at the wire tip the material transfer can be followed droplet by droplet. Short exposures freeze the motion, and the global shutter exposes the whole frame at one instant, so a droplet is not smeared across scan lines.
Pool Emittance at 1000nm
Molten steel radiates strongly in the near infrared. The ReconFlex™1920NA is built for that band, so the pool and the parts around it stay legible while the arc is burning — the tungsten, the filler rod and the pool surface are all readable in the same frame.
Visible-light cameras lose that detail to arc glare. Thermal cameras see the heat but not the geometry.
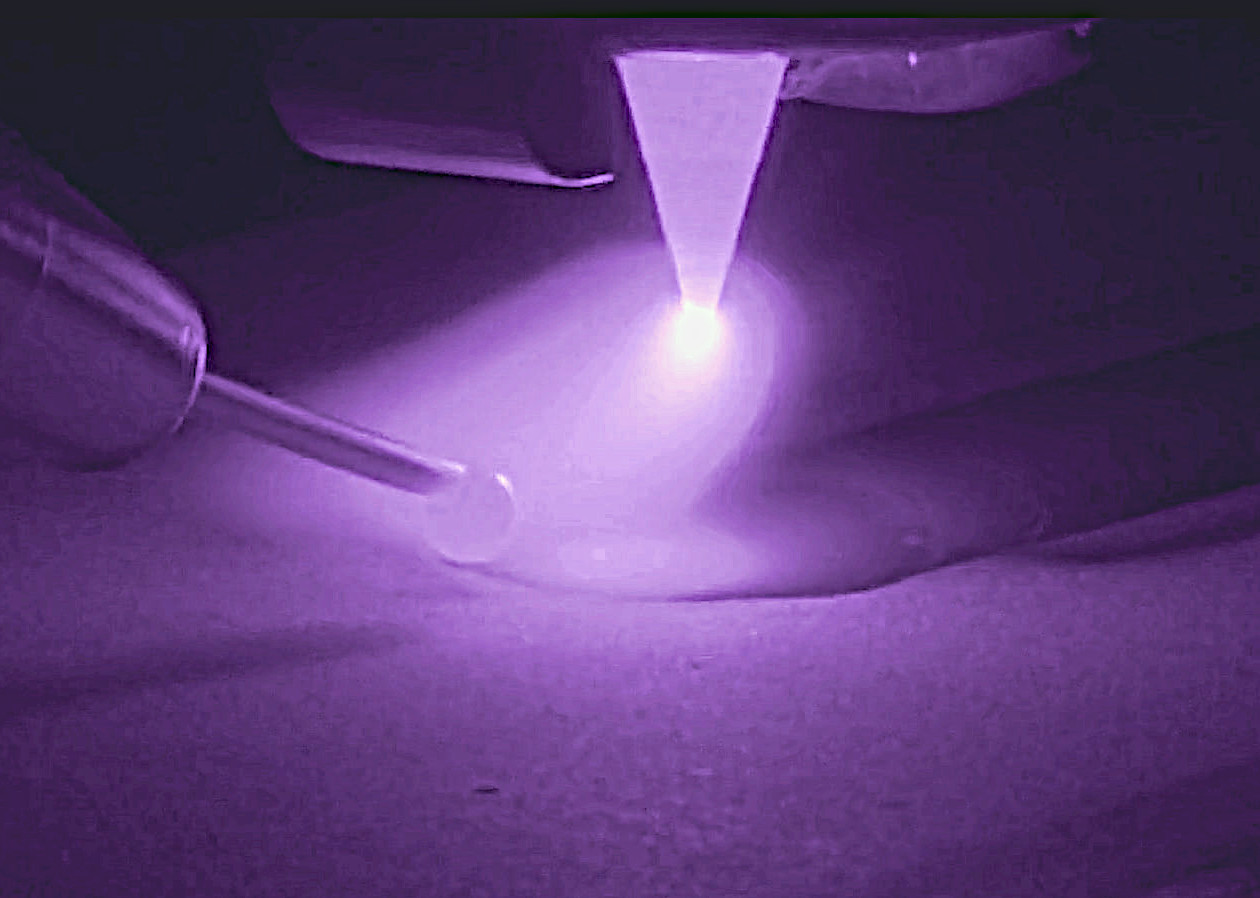
The scene above under one of the software colour maps. The recording is unchanged — only the mapping differs.
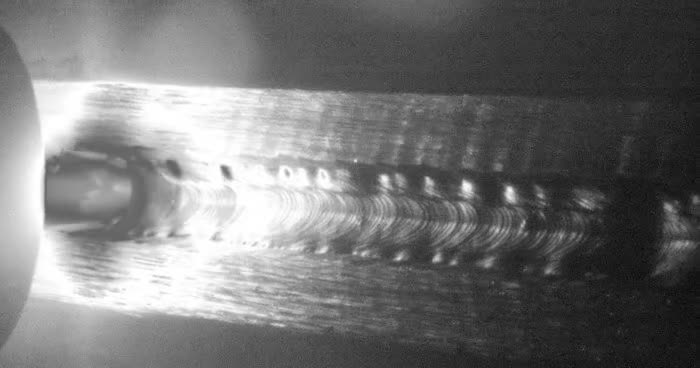
The solidified seam trailing the arc, from the same recording.
One Stream: from Arc to cooled Seam
Up to 140 dB of dynamic range, shaped by a seven-point spline tone curve, lets the arc and the cooled seam sit in one exposure. HDR runs at up to 100 fps; where speed matters more than range, plain 8-bit or 12-bit readout goes far higher. Either way you do not need a second camera, a second pass or a different filter to inspect the result.
Exposure runs from 4 µs to 200 ms, and the software adjusts frame rate to exposure automatically, so the settings stay valid when the process changes.
The Arc Trace: Two Cameras but One Timeline
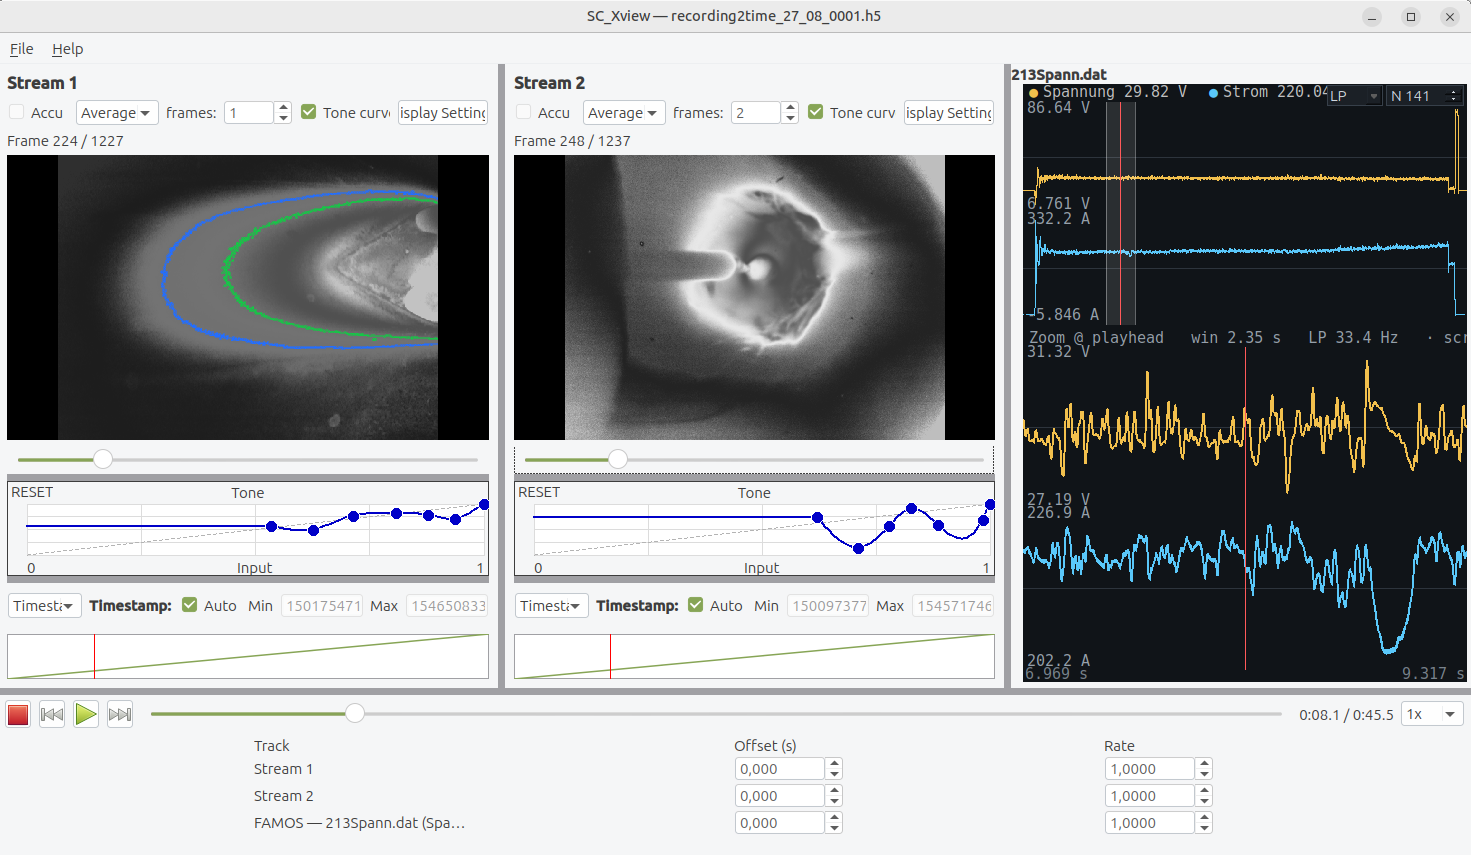
The weld camera software plays synchronised camera streams against the measured welding voltage and current. Timestamps are matched to the microsecond, so a current dip and the frame it belongs to sit at the same position on the timeline. Isotherm contours are drawn live over the image, and any stream can be recoloured without touching the recording.
Grayscale
False Colour
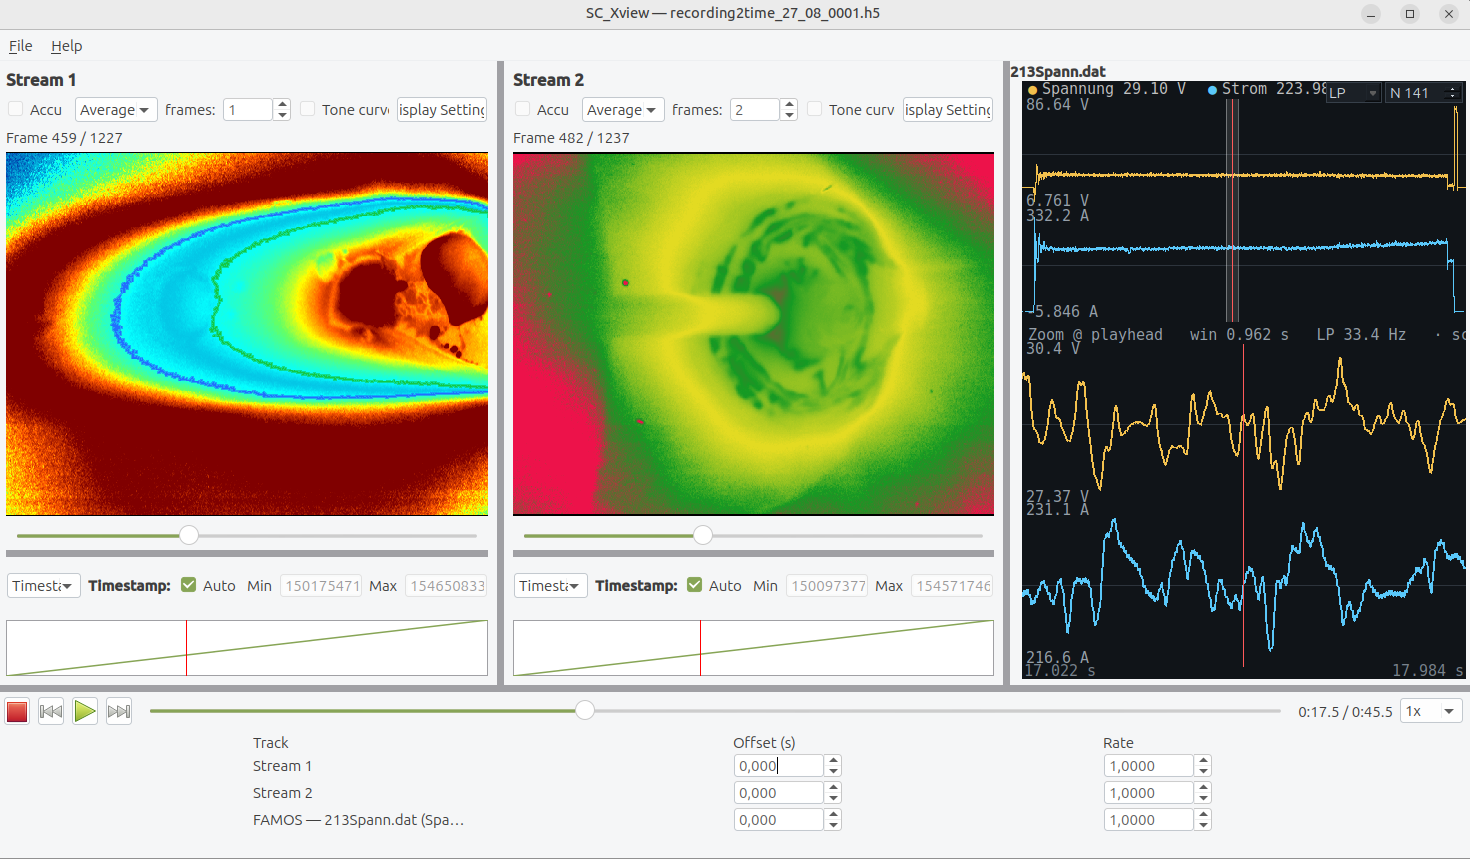
The same recording, switched between mappings. Isotherm contours and the voltage and current traces are unaffected.
Outer isotherm contour
Outer isotherm contour
Welding voltage
Welding current
Recording
Streams to HDF5, or to MPEG with the AV1 or FFV1 codec when you need a lossless archive.
Image Control
HDR mode up to 140 dB at up to 100 fps, seven-point spline tone mapping, free colour mapping, and automatic frame-rate control tied to exposure time.
Measurement
Temperature-zone detection, automatic determination of welding speed, and weld parameter inspection run on the live stream.
Analogue Channels
Voltage and current are digitised in the camera electronics and carry the same time base as the images — no external synchronisation box.
Technical Specifications
| Parameter | ReconFlexTM 1920NA | ReconFlexTM 800NA |
|---|---|---|
| Sensor Technology | CMOS, Global Shutter | CMOS, Global Shutter |
| Optical Format | 2/3" | 1/1" |
| Resolution | 1920 x 1440 (2.8MP) | 800 × 600 (0.48MP) |
| Pixel Size | 4.5μm x 4.5μm | 4.5μm × 4.5μm |
| Peak Sensitivity NIR | 1000nm (NIR) | 1000nm (NIR) |
| Spectral Sensitivity NIR | 700-1250nm | 700–1250nm |
| Dynamic Range (native) | 80dB | 80dB |
| Dynamic Range (HDR Mode) | up to 140dB tone mapped | up to 140dB tone mapped |
| Max. Frame Rate (8-bit) | 409fps (full frame) | 1000+fps (RoI) |
| Max. Frame Rate (12-bit) | 231fps (full frame) | 650+fps (RoI) |
| Read Noise | ≤ 4e⁻ | ≤ 6e⁻ |
| Exposure Time | 4μs – 200ms (up to 10s) | 4μs – 200ms (up to 10s) |
| Output Formats | 8-bit, 12-bit, 16-bit (raw or subset) | 8-bit, 12-bit, 16-bit (raw or subset) |
| ADC Input (external) | ±10V, 16-bit | ±10V, 16-bit |
| Data Interfaces | USB 3.0 + 1GigE Ethernet | USB 3.0 + 1GigE Ethernet |
| Trigger I/O | TTL (SMA connectors) | TTL (SMA connectors) |
| Lens Mount | C-mount | C-mount |